
- Home
- Products
- Hot
- About Us
- Services
- Industry
- Contact
Views: 0 Author: Site Editor Publish Time: 2026-10-13 Origin: Site


Strict air purity requirements dominate the food, beverage, pharmaceutical, and electronics manufacturing sectors. Even a microscopic drop of oil carryover causes catastrophic product contamination. Such events ruin brand reputations and trigger massively expensive product recalls. Transitioning to a water-injected system completely eliminates this lubrication risk from the compression chamber. However, this facility upgrade introduces complex new variables into your daily operations. You must now actively manage reverse osmosis water quality, monitor airend material durability, and adhere to entirely different lifecycle routines. This comprehensive guide moves far beyond superficial marketing brochures. It delivers a rigorous, evidence-based evaluation framework for facility engineers and buyers. You will learn exactly how to analyze critical technical data before finalizing any major procurement decision.
Water acts as a superior cooling agent compared to air. It absorbs heat rapidly during the compression process. This thermal dynamic enables near-isothermal compression. Because the temperature stays remarkably stable, the compressor requires significantly less energy to compress the air. You gain a massive thermal efficiency advantage over traditional dry oil-free screw compressors. Dry screws run extremely hot and often require two separate compression stages just to manage the heat. However, introducing liquid into the compression chamber brings distinct corrosion risks.
You must carefully evaluate this technology through a practical lens. Identify exactly when the initial capital expenditure justifies the transition. Facilities typically see success when lower running temperatures and reduced energy consumption align with high-demand production schedules. If your plant runs continuously, the energy savings quickly offset the initial equipment price.
Best Practice: Always conduct a risk mitigation assessment before finalizing your choice. Selecting incorrect parameters introduces severe operational hazards. For example, stagnant water circuits encourage microbial growth. Poor material selection leads to premature rotor failure due to rust. You must thoroughly understand your facility's ambient environment and technical capabilities before proceeding.
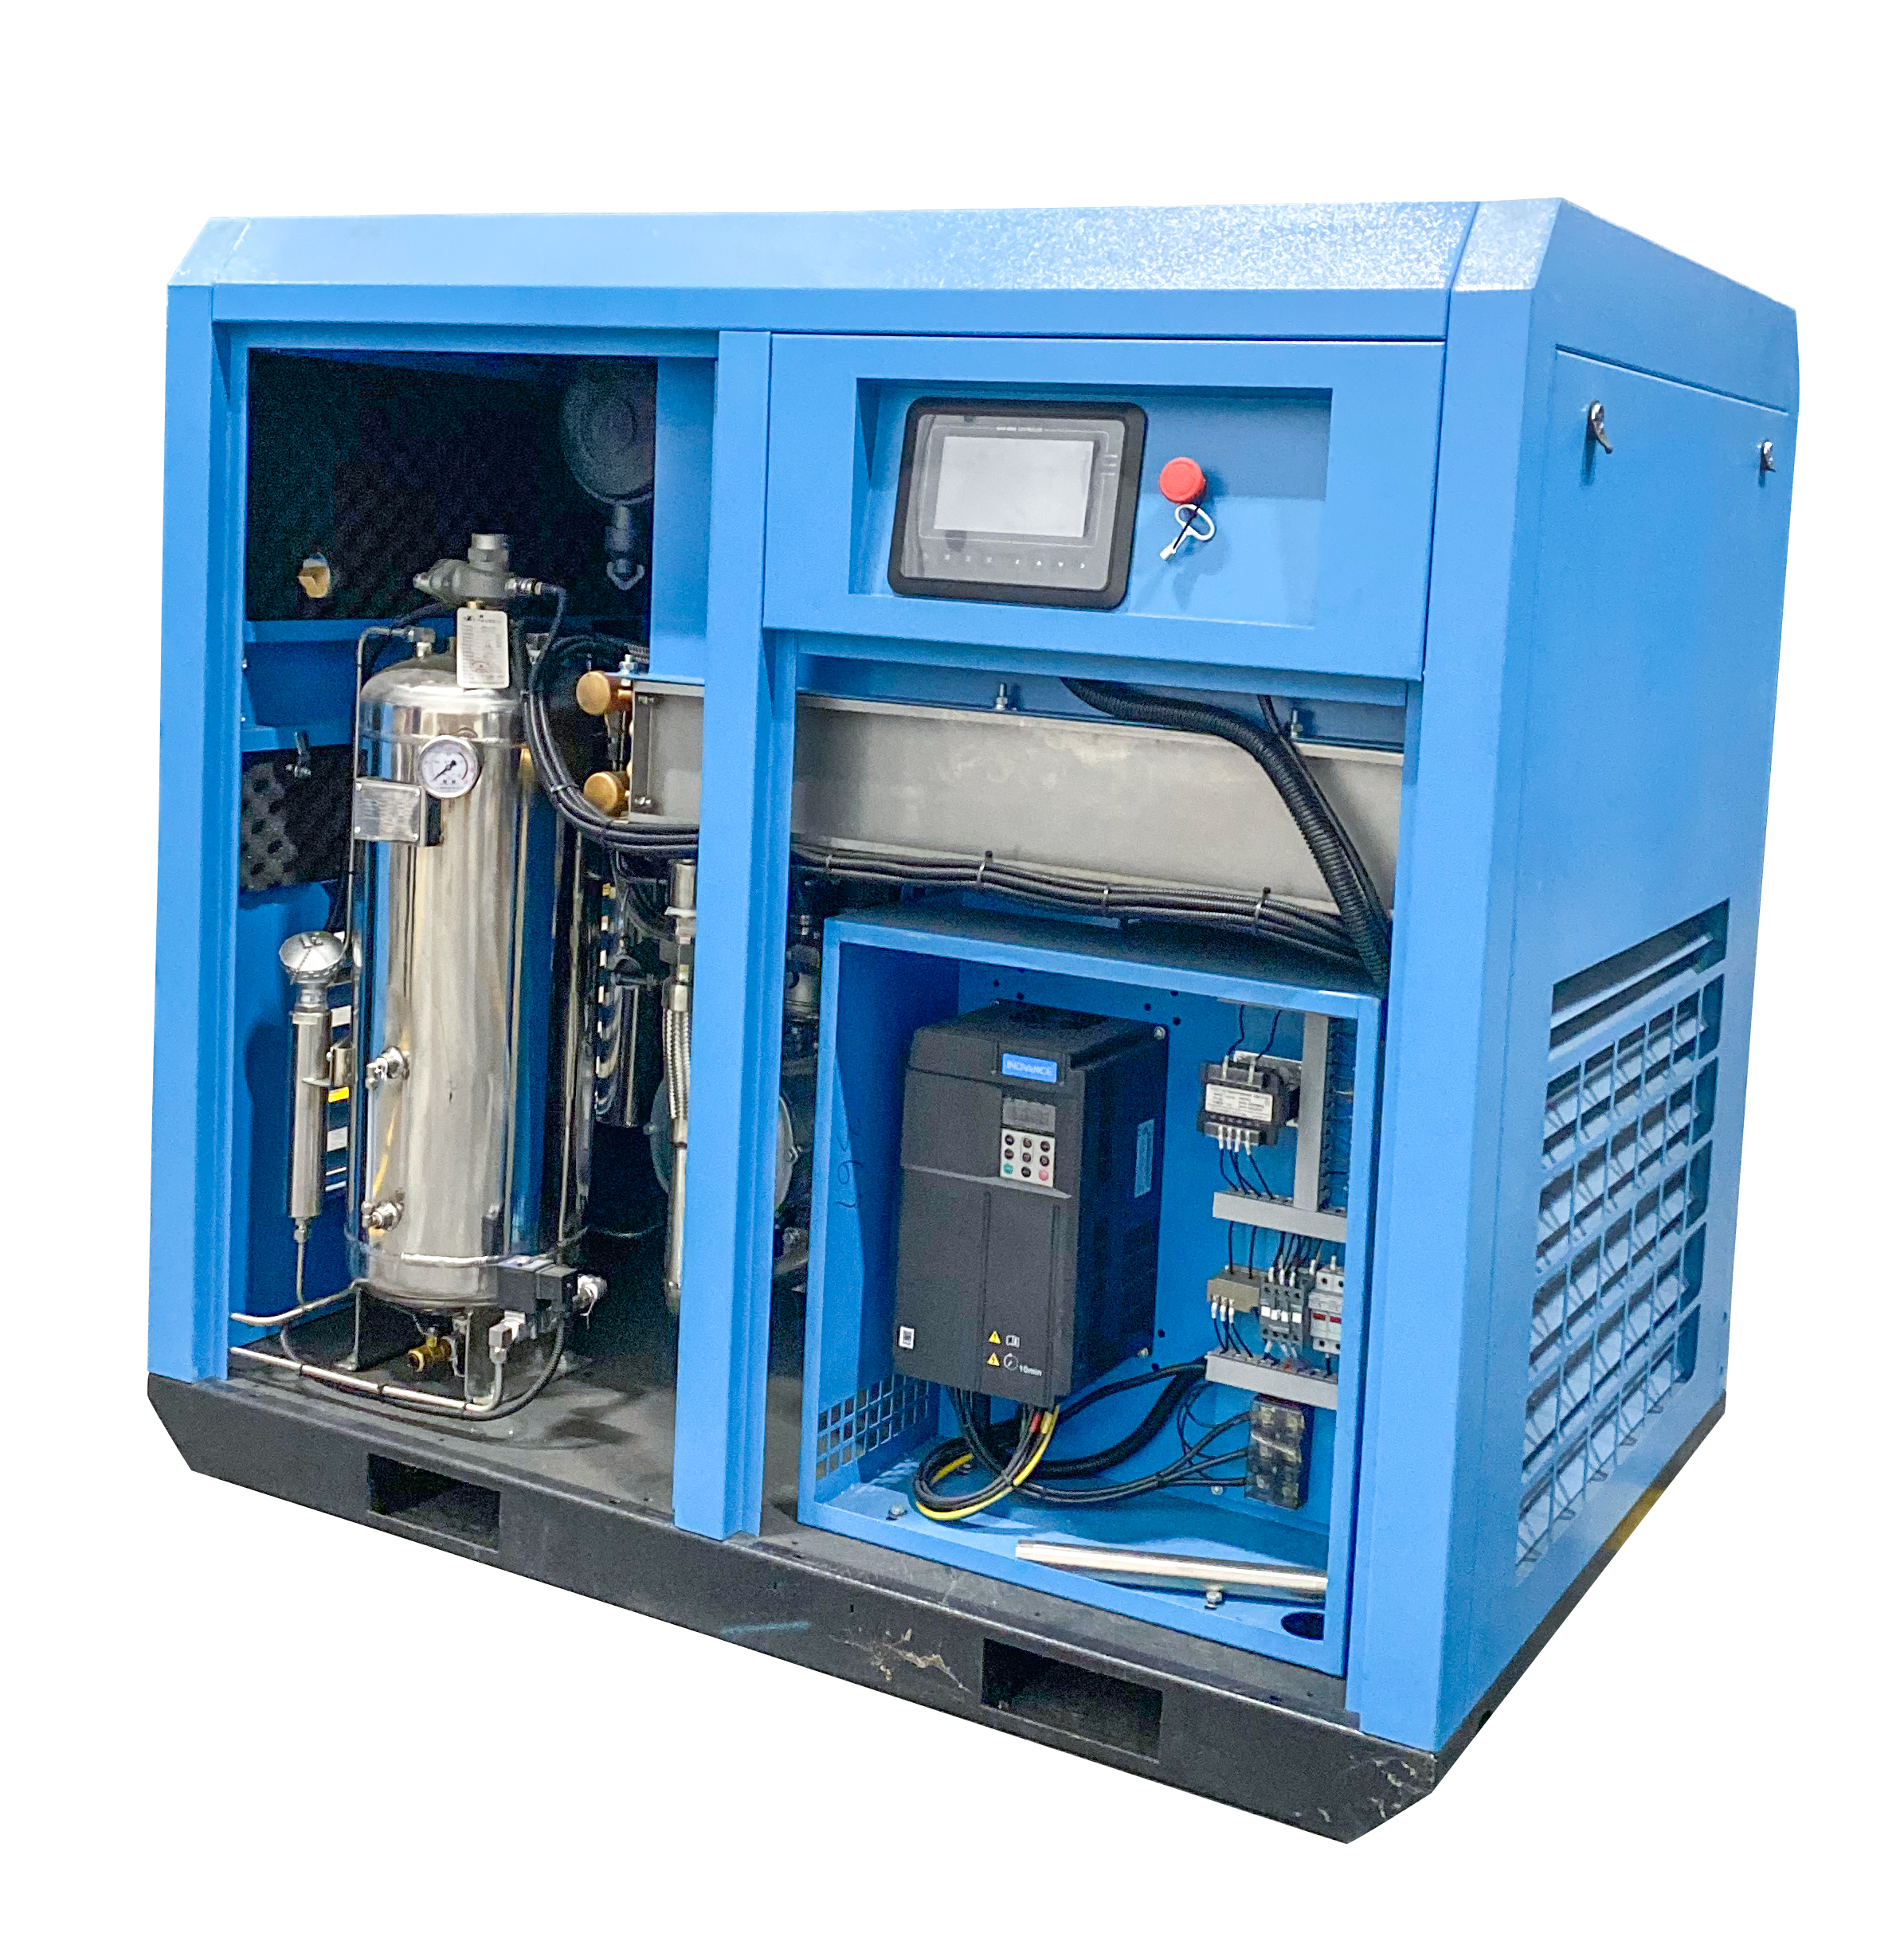
Manufacturers often highlight best-case maximums on their sales brochures. You must ignore these peak numbers. Instead, instruct your buying team to evaluate Free Air Delivery (FAD) at your specific required pressure point. Pressure drops occur naturally across piping networks, filters, and dryers. If you size the machine based purely on maximum output, you will experience dangerous pressure shortages at the production line.
Common Mistake: Buying a compressor rated for 125 PSI when the plant only needs 90 PSI. Compressing air to a higher pressure than necessary wastes enormous amounts of electrical energy.
Specific power represents the true gold standard of efficiency measurement. We define specific power as kilowatts consumed per 100 cubic feet per minute of air produced (kW/100 CFM). A lower specific power number indicates a more efficient machine. You must demand this exact metric from every vendor.
Comparing Variable Speed Drive (VSD) performance curves remains absolutely critical. The core water lubricated compressor specifications often hinge on how well the VSD motor responds to fluctuating plant demands. Look closely at the efficiency ratings across the entire speed range, not just at 100% load.
Skeptical Buyer Tip: Always verify if the stated efficiency includes the power draw of ancillary components. Cooling fans and internal water circulation pumps consume significant electricity. Some manufacturers exclude these parasitic loads to artificially lower their published specific power numbers.
The turndown ratio defines the operational flexibility of the compressor. It represents the range between maximum output and minimum output before the machine shuts down. A wider turndown ratio in a VSD model prevents highly inefficient start/stop cycles.
When plant demand drops during a night shift, a compressor with a wide turndown ratio simply slows its rotors. It continues delivering air smoothly. Conversely, a machine with a narrow ratio will shut off completely. It must then restart violently when demand returns. These constant restarts cause massive electrical spikes and accelerate mechanical wear on the motor bearings.
Long-term reliability hinges entirely on superior corrosion resistance. Since water directly contacts the moving parts, standard carbon steel fails rapidly. Manufacturers use different proprietary solutions to solve this chemical challenge.
You cannot use standard municipal tap water in these highly engineered machines. Tap water contains dissolved minerals like calcium and magnesium. These minerals rapidly form scale on the rotors, destroying the tight internal clearances. Most industrial units strictly require Reverse Osmosis (RO) or demineralized water.
You must also investigate the automated water flushing cycles. Ask the vendor how the machine handles idle periods. Quality units automatically drain and replace their internal water supply during downtime. This critical automated step prevents bacterial growth, algae formation, and internal scaling when the rotors sit still.
Engineers generally choose between two distinct bearing lubrication methods. Both approaches carry different maintenance implications.
Water-lubricated hydrodynamic bearings utilize the existing internal water circuit for lubrication. They simplify the overall mechanical design. However, they demand absolute water purity to prevent microscopic scoring on the bearing surfaces.
Alternatively, sealed, grease-lubricated bearings sit completely outside the compression chamber. Atmospheric seals separate them from the water zone. This isolation protects the bearings from moisture contamination. It often extends the mechanical lifespan of the rotational assembly, provided the seals remain intact.
A reliable water-lubricated oil-free compressor demands a strict adherence to its service schedule. You must prepare your maintenance team for these specific milestones.
At the 4,000-hour mark, technicians typically perform basic preventative care. They inspect air intake filters, replace the primary water filters, and check the RO membrane integrity. This ensures the fluid circuit remains completely uncontaminated.
The 8,000-hour service requires a more invasive inspection. Technicians will clean the internal water separator, test the automated flush valves, and inspect the main motor bearings. They also analyze the drive couplings for premature wear.
The 20,000-hour benchmark often triggers a major preventative overhaul of the peripheral systems. You will likely replace the atmospheric seals, upgrade the internal circulation pumps, and perform a comprehensive vibration analysis on the airend housing.
Airend longevity serves as a primary evaluation metric for any facility engineer. How many hours can the machine run before a full airend rebuild becomes necessary? You must compare manufacturer guarantees directly.
Some builders offer standard 5-year airend warranties. Others provide comprehensive 10-year guarantees, provided you maintain strict water quality standards. Because water reduces internal thermal stress, a well-maintained water-injected airend often outlasts a dry screw equivalent. Always demand clarity on exactly what operational conditions void these warranties.
You must accurately map out the ongoing physical replacement parts. Traditional compressors require massive volumes of synthetic oil and expensive air-oil separators. Your new system eliminates those specific items, but introduces new requirements.
You will frequently purchase replacement water filters. You must also maintain the external RO water generation system, which requires periodic membrane replacements. Air intake filters remain a standard requirement. By mapping these physical components upfront, you prevent surprise budget shortages during your annual maintenance cycles.
Maintenance Component Comparison| Component Category | Traditional Dry Screw (Oil-Lubricated) | Water-Lubricated Oil-Free |
|---|---|---|
| Primary Fluid | Synthetic Oil (High replacement volume) | RO Water (Low replacement volume) |
| Separation Elements | Air/Oil Separator required | Water separator (No specialized elements) |
| Cooling System | Oil coolers and fans | Water acts as inherent coolant |
| Internal Bearings | Oil-bathed | Sealed grease or water-hydrodynamic |
Never accept marketing claims at face value. You must demand rigorous, independent documentation before moving forward with a purchase.
First, request the independent TUV Rheinland certification for ISO 8573-1 Class 0. This globally recognized document proves the machine delivers 100% oil-free air under strict testing conditions. Self-certified manufacturer letters hold no weight in critical manufacturing environments.
Second, require CAGI (Compressed Air and Gas Institute) data sheets. CAGI provides standardized, third-party verified testing formats. These sheets allow you to verify performance metrics, FAD, and specific power claims accurately across different brands.
A brilliant machine fails instantly without competent local support. You must evaluate the local availability of factory-trained technicians. Water-injected systems require entirely different diagnostic skills than standard oil-flooded models.
Ask the vendor how many local technicians hold specific certifications for water-lubricated equipment. If they plan to dispatch a general mechanic, you risk prolonged downtime during complex troubleshooting scenarios.
We highly recommend conducting a comprehensive baseline air demand audit on your current facility. You should execute this step before locking in any final water lubricated compressor specifications.
Selecting the right water-lubricated oil-free compressor requires balancing near-isothermal energy efficiency with rigorous, corrosion-proof engineering. You successfully eliminate the threat of oil contamination, but you take on the responsibility of managing internal fluid purity. Buyers must carefully weigh these strict water quality management requirements against the substantial long-term energy savings.
To ensure operational success, never skip the independent verification phase. Insist on reviewing verified CAGI data sheets to confirm specific power metrics. Furthermore, always complete a comprehensive site air audit with a certified engineer. Gathering actual flow data before submitting your final RFQ guarantees you purchase a properly sized, highly efficient machine built to support your specific production goals.
A: Water sealing and cooling allow for lower rotor RPMs and near-isothermal compression. Because water removes heat so effectively during the process, these units generally achieve 10-15% better energy efficiency than a standard two-stage dry screw compressor.
A: Most industrial units strictly require RO (Reverse Osmosis) or highly filtered, demineralized water. Using purified water prevents internal scaling, harmful mineral deposits, and rapid metal corrosion within the compression chamber.
A: Yes, microbial growth occurs if the water remains stagnant. High-quality systems mitigate this risk by using automated water flushing routines, strict temperature controls, and sometimes UV treatment to prevent bacteria and algae formation during off-cycles.
A: With proper water quality management and strict adherence to maintenance intervals, high-quality stainless steel or ceramic airends offer exceptional durability. They can frequently exceed 40,000 to 50,000 operating hours before requiring a major factory overhaul.


